Cold Room Indoor Unit
Description
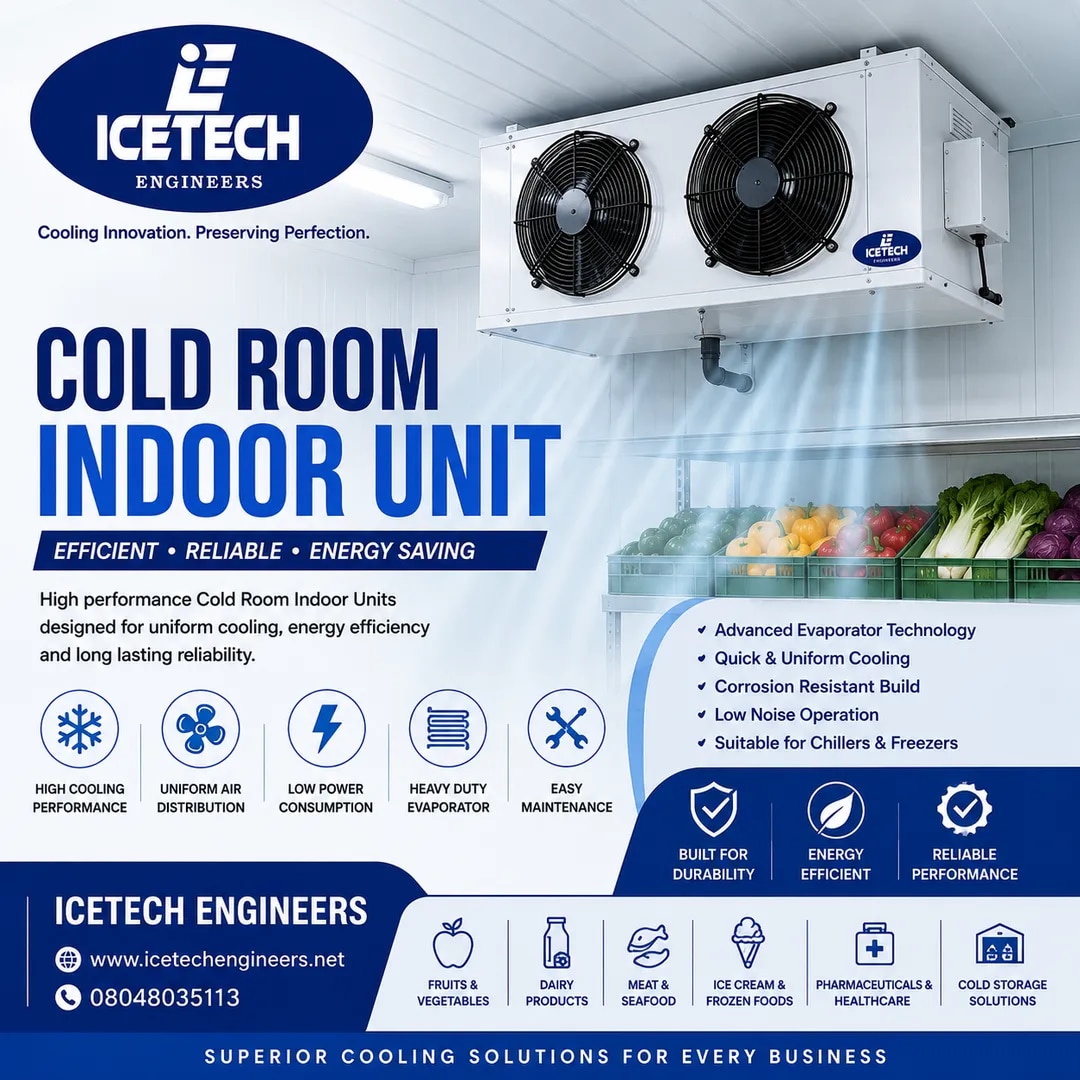
ICETECH ENGINEERS is a leading manufacturer and supplier of premium-quality Cold Room Indoor Units designed to deliver efficient and uniform cooling for commercial and industrial cold storage applications. Our indoor evaporator units are engineered with advanced heat exchange technology, high-performance fans, and corrosion-resistant components to maintain precise temperature control while maximizing energy efficiency.
Designed for seamless integration with walk-in chillers, walk-in freezers, cold storage rooms, fruit ripening chambers, and pharmaceutical cold rooms, our indoor units ensure consistent airflow, rapid cooling, and reliable operation for temperature-sensitive products.
Whether you require a standard or customized refrigeration solution, ICETECH ENGINEERS offers durable and energy-efficient Cold Room Indoor Units that support uninterrupted cold chain operations.
Why Choose ICETECH ENGINEERS Cold Room Indoor Units?
Our indoor evaporator units are manufactured using high-quality materials and advanced refrigeration technology for dependable performance.
High-efficiency evaporator coil design
Powerful airflow for uniform cooling
Energy-efficient fan motors
Corrosion-resistant construction
Low-noise operation
Rapid and consistent cooling performance
Digital temperature control compatibility
Easy installation and maintenance
Long service life
Suitable for commercial and industrial refrigeration systems
Applications of Cold Room Indoor Units
Our Cold Room Indoor Units are widely used in:
Cold Storage Rooms
Walk-In Chillers
Walk-In Freezers
Multipurpose Cold Storage
Fruit Ripening Chambers
Ice Cream Cold Storage Rooms
Pharmaceutical Cold Rooms
Dairy Processing Plants
Meat & Poultry Storage
Seafood Cold Storage
Hotels & Restaurants
Supermarkets & Hypermarkets
Food Processing Industries
Cold Chain Warehouses
Advanced Features
Every Cold Room Indoor Unit manufactured by ICETECH ENGINEERS is equipped with modern refrigeration features for reliable cooling.
High-performance evaporator coils
Heavy-duty axial fan motors
Uniform air distribution
Fast cooling technology
Automatic defrost compatibility
Low power consumption
Premium copper tube and aluminum fin construction
Hygienic and corrosion-resistant finish
Digital monitoring compatibility
Minimal maintenance requirements
Benefits of Cold Room Indoor Units
Installing a premium-quality indoor refrigeration unit provides several operational benefits.
Maintains consistent storage temperatures
Ensures even cooling throughout the cold room
Extends shelf life of stored products
Reduces temperature fluctuations
Improves refrigeration efficiency
Lowers electricity consumption
Minimizes product spoilage
Supports uninterrupted cold chain operations
Reduces maintenance costs
Enhances overall system performance
Customized Cold Room Indoor Unit Solutions
Every cold storage project has unique refrigeration requirements. ICETECH ENGINEERS offers customized indoor units based on:
Cold room dimensions
Required cooling capacity
Operating temperature
Product storage requirements
Airflow design
Industrial or commercial applications
Future expansion plans
Our experienced engineering team provides complete support from product selection and system design to installation, testing, commissioning, and maintenance.
Industries We Serve
Our Cold Room Indoor Units are trusted across multiple industries, including:
Food Processing Industry
Cold Storage Warehouses
Agriculture & Horticulture
Dairy Industry
Pharmaceutical Industry
Ice Cream Manufacturing
Frozen Food Industry
Seafood Processing
Meat Processing Plants
Hotels & Restaurants
Supermarkets
Cold Chain Logistics
Why ICETECH ENGINEERS?
ICETECH ENGINEERS is committed to delivering advanced refrigeration solutions that combine innovation, durability, and energy efficiency. Our Cold Room Indoor Units are manufactured using premium components and modern engineering practices to ensure long-lasting performance and reliable cooling. From design and manufacturing to installation and after-sales support, we provide complete refrigeration solutions tailored to your business needs.
Frequently Asked Questions (FAQs)
1. What is a Cold Room Indoor Unit?
A Cold Room Indoor Unit, also known as an evaporator unit, is installed inside the cold room to circulate chilled air and maintain a consistent storage temperature.
2. What is the function of a Cold Room Indoor Unit?
It absorbs heat from inside the cold room and distributes cooled air evenly, ensuring stable temperatures for stored products.
3. Which applications require Cold Room Indoor Units?
They are commonly used in walk-in chillers, walk-in freezers, cold storage rooms, fruit ripening chambers, pharmaceutical storage, dairy plants, and food processing facilities.
4. Are ICETECH ENGINEERS Indoor Units energy efficient?
Yes. Our indoor units feature energy-efficient fan motors and advanced evaporator designs that deliver high cooling performance with reduced power consumption.
5. Can the Indoor Unit be customized?
Yes. We provide customized indoor units based on cooling capacity, room size, airflow requirements, and specific industry applications.
6. What materials are used in the evaporator?
Our indoor units are built with high-quality copper tubes, aluminum fins, durable fan motors, and corrosion-resistant housings for maximum efficiency and longevity.
7. Do you provide installation and maintenance services?
Yes. ICETECH ENGINEERS offers complete installation, testing, commissioning, preventive maintenance, and technical support throughout India.
8. Are the Indoor Units suitable for low-temperature applications?
Yes. Our indoor units are designed for both chiller and freezer applications, ensuring reliable performance across a wide temperature range.
9. How often should the Indoor Unit be serviced?
Routine maintenance every 3–6 months is recommended to maintain optimal airflow, cooling efficiency, and equipment life.
10. Why choose ICETECH ENGINEERS for Cold Room Indoor Units?
ICETECH ENGINEERS delivers customized, energy-efficient, and durable Cold Room Indoor Units backed by expert engineering, premium-quality manufacturing, and dependable after-sales service.